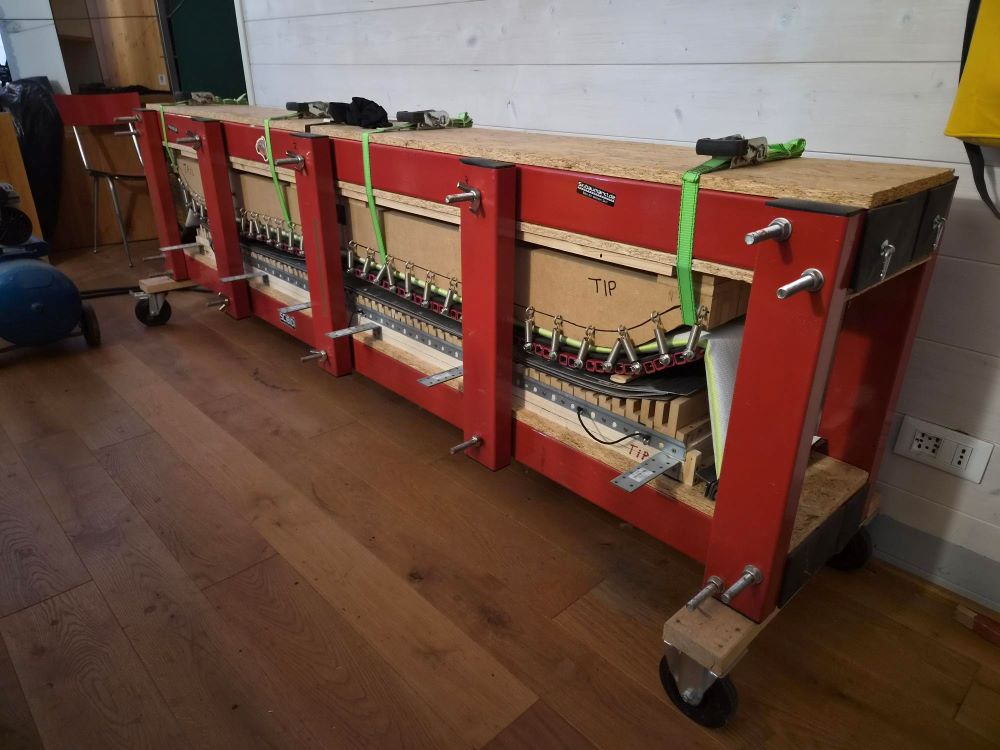
i’ve build my press in 2022, i’ve build my first two pair of skis with vacuum press but they didn’t last long, the frame is made in iron square tubing(3+3 top-bottom 100x100mm 2200mm long), vertical element rectangular iron tubing(100x50mm, 5 in the back bolted and 5 in the front 2 bolted 3 removable for insert the cassette-ski in), the frame is bolted together with treaded bar and bolt m12(exept the 3 front removable vertical element i’ve used “butterfly” bolt), 4 caster wheel for moving,clening, maintenance
top mold cut in two part for shorter-longer/more-less tail rocker ski (insert in in the middle) fixed with ratchet strap to the frame, hooks for “carpet” springs
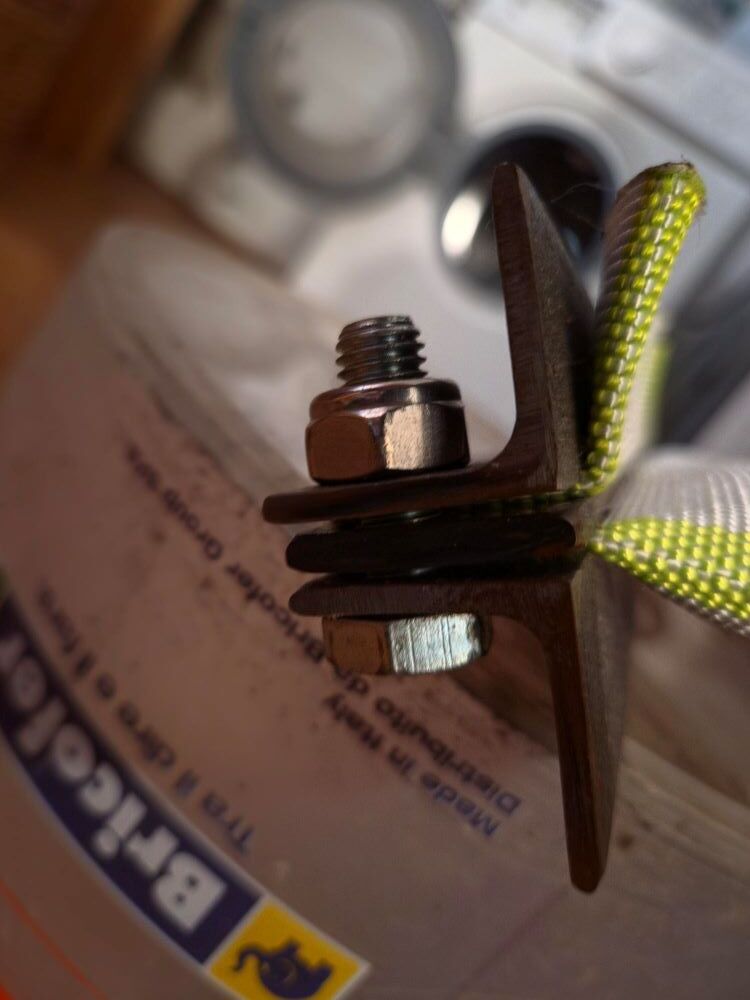
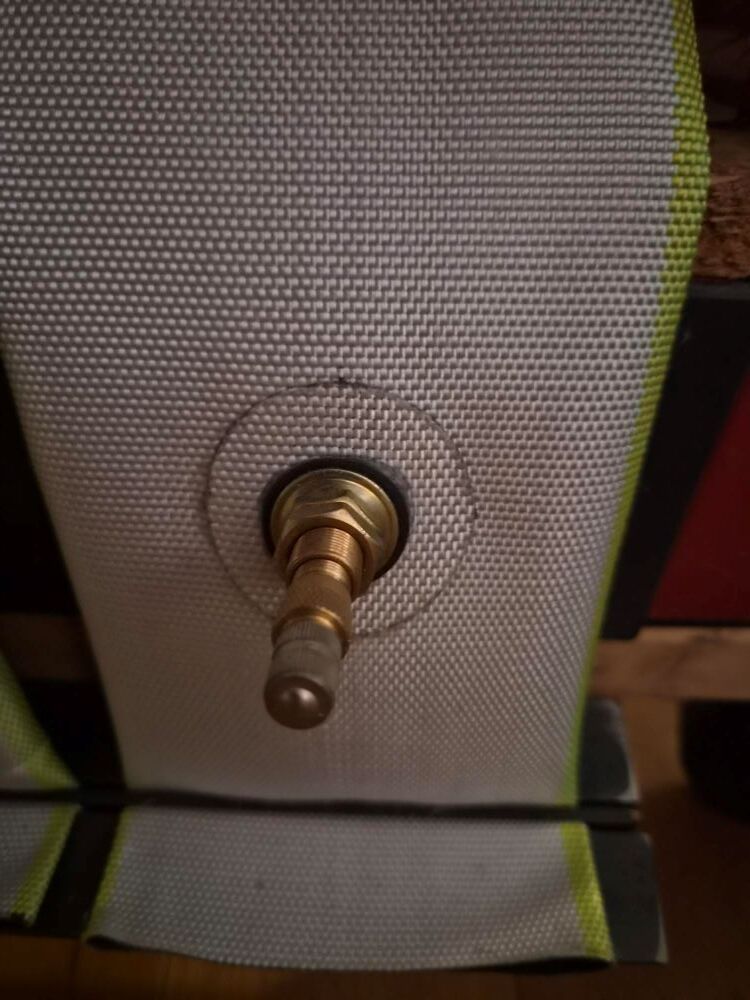
bladder 2X3 inch fire hose clamped as in the photo(i’ve add glue superattak flex after the fold inside for air tight), with tractor tire valve(i’ve add a “washer” of fire hose fabic glued with superattak flex for more thickness-better clamping)
iron “carpet” square profile 3mm wall “stiched” together with steel cable(a washer between each section) small threaded 1 every 3 bar+washers to hold the spring connected to top mold(hooks)
neoprene
top two layer cassette 2mm aluminium sheet+heatmat(not showed)+2mm aluminium sheet+release ptfe film (no wax, easier cleaning)
“SKI”
bottom two layer cassette 3mm Al sheet(layup) with release ptfe film + neoprene + 2mm Al sheet
90° slot mold (i’ll post a specific topic), 6 metal plate to estract-insert the mold and easier cassette insertion
plywood spacer with rail for mold alignement
osb with rail for mold alignement
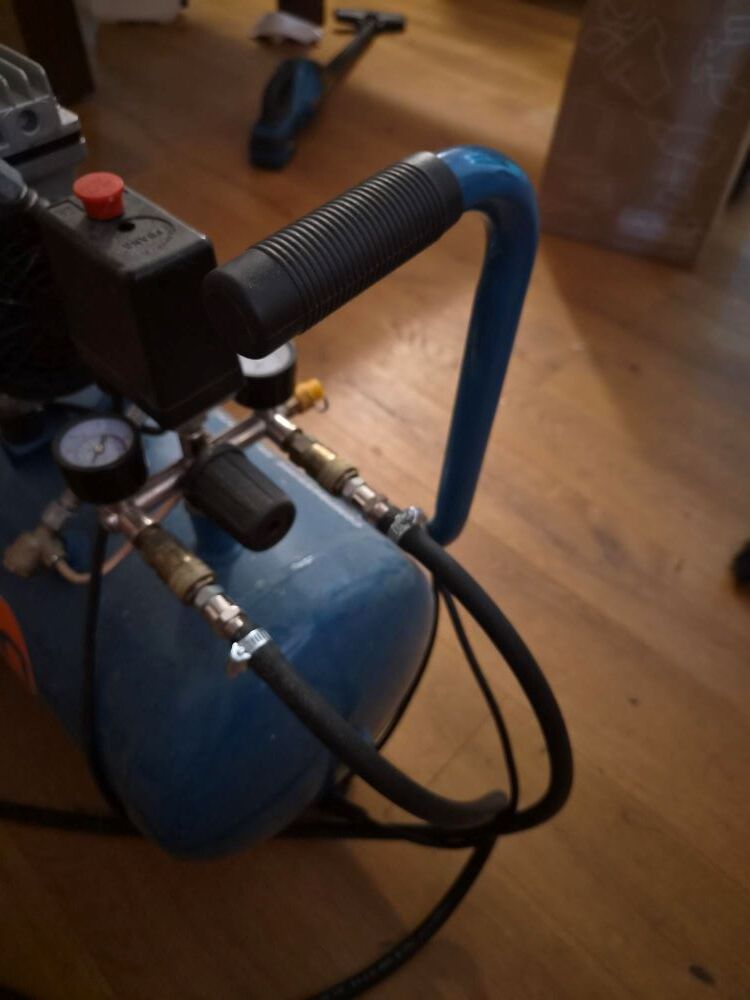
i use a cheap air compressor with 2 air outlet, two air compressor gun with digital gauge and threaded connection to connect the valve, i press at 5 bar for a week, heating(only at the top) at 50°c for 5 hours after layup,
i didn’t used I beam for low availability, hard drilling (no plasma or oxy),price
i zip-tie the top-bottom cassette with 10 holes for each top-bottom Al sheet cassette after layup
during press it deform (bows) a little, maybe i will upgrade with more vertical element…
with deep profile ski i add a wood spacer tip-tail under the “carpet” for better pression in the lower-deeper area
no bottom heatmat to aviod ptex and edges deformation, opinion abut this?
heatmat: i prefer like that,i think the steel edge can expand during heating from beneath in a flat cassette, 0,5 mm deformation could potentially move even if it’s glued to the base (in factory-professional ski building they can afford high temparature due to 3d cassette thet keep everything together orizontally i think even 1mm of deformation is compensated by the 3d cassette), leave a piece of cut out base in the sun for few ours it will deform in some way imagine blasting heat from underneath, the press do his work limiting that but i build 1-2 pair of ski a year and i’m not willing to waste any material for overheat.
i also think that the epoxy slowly move between base and edge for a better glueing during press if i heat the epoxy it accellerate the cure and became less fluid and doesn’t reach every spot.
i’m also economic motivated by non buying a second mat, i’ve bought the mat from alibaba for about 150€, i save the money to buy bindings or something else
press timing: i prefer to press for a week (5 days or more) beacase epoxy phase are: liquid 45min - gel about 2-5 hour(heat dependent)- cured 12-24 hours -fully cured 24-74h or more. i use Sei Whale Universal All-purpose resin SLOW
every shop/tutorial i’ve read say that you don’t test flex your ski for at least 5 days after press so i keep in the press and forget about it, in an industrial enviroment you have to optimize work time to reduce money waste, i don’t care about that, it’s a waste of money anyway!!! the full process take me from the ski resort close till it’s open again!!! i don’t sell ski i build ski!!!
i repeat i’m not an engineer, i didn’t test anything statically, i base these opinion by belly!!! the only opinion i trust is by my ski-man when he flat the base: flat=good/not flat=not good, the other test i make is under my foot when i ski it! i’m not a ski teacher, never race-ski, but i love skiing and i ski the most as possible, i don’t even give my ski to try to somone else, i don’t want to break his knees!!!
What a beautiful press. Thanks for sharing. I see a few places to upgrade mine. I have bungee cords pulling up my cat track, but I need to upgrade to some springs. I have had issues with over-camber/de-camber when heating only from one side if I use a full titanal sheet. All my lightweight skis with just glass and carbon maintain their camber well with one sided heat from above. I want to buy a second blanket and try even heat top and bottom with titanal and see if I can get a ski to come out and stay like the mold. I’ve let them cool in the press for days, but they still warp in the direction of whichever side I applied the heat.
i’ve had the same problem with titanal… i’m building free titanal ski for carving, with ash wood core with 2 UD carbon fiber stripes between the central wood strips…i’ll post some pics soon!
I always assumed the entire layup is getting up to the temperature of the heater anyways.
I think the difference in under/over camber or rocker comes from the epoxy curing unevenly on the top or bottom first.
For what its worth, even in mass production, skis do not come out 1:1 to the mold. Apparently to get 1:1 to mold you have to do a slow ramp up in temp, let fully cure, then slowly ramp down under pressure.
And to your point, mass production doesn’t allow time for that obviously.
I use top heat as well. This is purely anecdotal and not truly tested out but I have found that the stiffer the ski, the closer it comes out to the actual mold… which is weird? I use fiberglass only.
i check temp with laser thermometre, top cassette is always hotter than bottom even after hours of heat, more difference underfoot (thicker) less tip tail (shallower), wood and glassfiberare termic isolant anyways…i use only quad glassfiber(0°/90°/±45°)650g/mq